A guide on the key brazing mistakes and some of the most common errors in industrial brazing PLUS actions to prevent them.
 Brazing is a reliable and widely used joining process in industry, but to achieve a quality joint, several parameters must be properly controlled.
The choice of brazing alloy, the use of flux, surface preparation, joint geometry and management of the thermal cycle are all factors that can influence the final result.
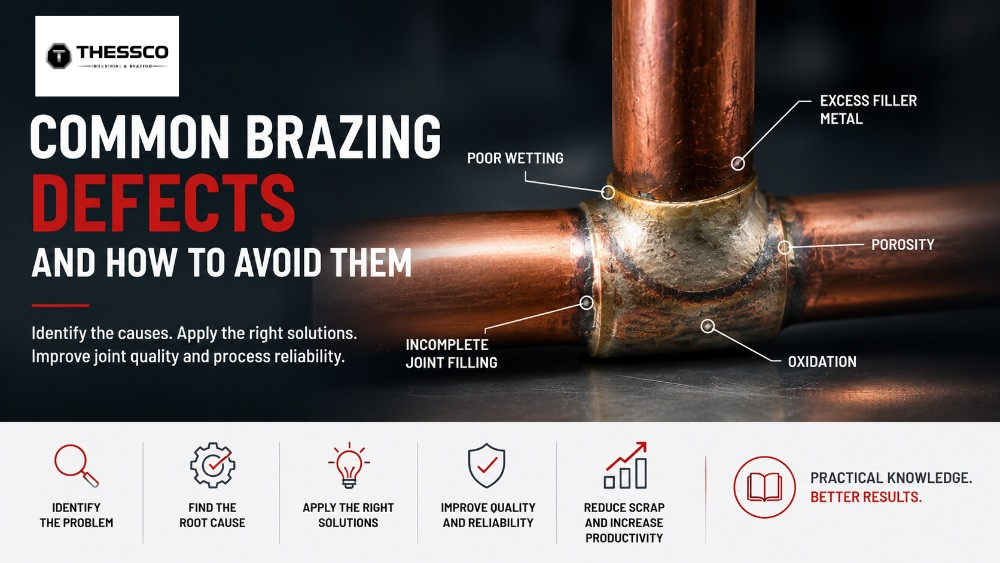
When any of these elements are not properly controlled, defects such as poor wettability, porosity, insufficient alloy penetration, oxidation or reduced joint strength may appear.
Analysing the type of defect and understanding its possible causes is therefore the first step to improving the quality of the brazing and making the process more stable and repeatable.
In this article, we analyse some of the most common errors in industrial brazing and the main actions to prevent them.
Top 10 Common Errors in Industrial Brazing
Insufficient Surface Preparation
One of the most common mistakes occurs even before starting the warm-up.
The surfaces to be brazed must be clean and free of contaminants that may hinder the wettability of the alloy.
Oils, greases, oxides, processing residues or other contamination can create a barrier between the base material and the brazing alloy.
Possible consequences
- poor wettability;
- uneven distribution of the alloy;
- failure to penetrate the joint;
- discontinuity in the brazed area;
- reduction in joint reliability.
How to avoid it
Before brazing, it is important to provide adequate surface preparation through degreasing, mechanical or chemical cleaning processes, depending on the materials and condition of the component.
The surface should be prepared as close to the time of brazing as possible, to prevent it from becoming contaminated or oxidized again.
Incorrect Joint Play
Brazing uses the phenomenon of capillary action to allow the molten alloy to penetrate the spaces between the components.
For this reason, the distance between the surfaces to be joined represents a fundamental parameter.
Excessive play can reduce the effectiveness of capillary action and require more solder.
Too little play, on the other hand, can prevent the alloy from penetrating the joint properly.
It is also important to consider that the clearance must be evaluated at the brazing temperature, taking into account the thermal expansion of the materials.
Possible consequences
- incomplete filling of the joint;
- non-uniform distribution of the alloy;
- reduction of mechanical resistance;
- greater variability between one component and another.
How to avoid it
The joint geometry must be designed considering:
- materials to be joined;
- brazing alloy used;
- thermal expansion coefficients;
- process temperature;
- geometry and dimensions of the components.
Correct joint clearance promotes uniform distribution of the alloy and contributes to the repeatability of the process.
Uneven Heating
One of the most common mistakes in flame brazing is concentrating the heat directly on the brazing alloy rather than uniformly heating the components being joined.
Under the right conditions, it is primarily the heat of the base materials that causes the alloy to melt and flow.
When the two components have different masses or thermal conductivities, heating management becomes even more important.
Possible consequences
- irregular alloy melting;
- poor penetration;
- localized overheating;
- increased oxidation;
- uneven joint quality.
How to avoid it
Heat must be distributed in a controlled manner, paying particular attention to parts with greater mass or greater capacity to dissipate heat.
In automated processes, precise control of the thermal cycle via induction or furnace can help significantly improve repeatability.
Overheating of the Joint
Raising the temperature too much will not improve the brazing.
Conversely, overheating can alter the behavior of the brazing alloy, increase the oxidation of the materials and compromise the effectiveness of the flux.
In fact, each alloy has its own melting range and recommended brazing temperature.
Possible consequences
- intense oxidation of surfaces;
- degradation of the flux;
- alteration of the alloy’s fluidity;
- worsening of the joint’s appearance;
- possible deterioration of the characteristics of the base materials.
How to avoid it
It is important to work within the thermal range specified for the alloy used and to limit the time spent at high temperatures.
The principle should be to use the heat necessary to obtain the correct flow of the alloy, avoiding excessive heat input .
Insufficient Temperature
The opposite problem can also compromise the result.
If the joint does not reach an adequate temperature, the alloy may begin to melt without reaching the conditions necessary for proper wettability and capillary diffusion.
Possible consequences
- alloy that remains concentrated in the application area;
- poor wettability;
- incomplete penetration;
- irregular joint;
- insufficient mechanical resistance.
How to avoid it
Before fully feeding the alloy into the joint, it is necessary to ensure that the components have reached an adequate and sufficiently uniform temperature.
Incorrect Choice of Brazing Alloy
Not all brazing alloys are suitable for all materials and all processes.
The selection must simultaneously consider:
- basic materials;
- brazing temperature;
- operating conditions of the component;
- mechanical stresses;
- warm-up technique;
- joint geometry.
For example, silver-based alloys offer high versatility and excellent wetting characteristics on numerous materials, while CuP and CuPAg alloys are widely used in copper brazing, particularly in the HVAC and refrigeration sectors.
Possible consequences of an incorrect choice
- poor wettability;
- inadequate process temperature;
- fragile joints;
- processing difficulty;
- insufficient performance under operating conditions.
How to avoid it
The alloy should be selected based on the application and not simply on the melting temperature or cost.
The most economical solution in terms of materials, in fact, does not necessarily coincide with the most efficient one considering the entire production process.
Incorrect use of the Deoxidizer
The brazing flux has the task of removing the oxides present on the surfaces and protecting them from new oxidation during heating, promoting the wettability of the brazing alloy.
An insufficient quantity, a flux not suitable for the process temperature or an uneven application can compromise the result.
Prolonged overheating can also reduce its effectiveness.
Possible consequences
- surface oxidation;
- difficulty in the flow of the alloy;
- insufficient wettability;
- irregular joints;
- residues that are difficult to remove.
How to avoid it
You need to use a deoxidizer:
- compatible with materials;
- suitable for brazing alloy;
- effective across the process temperature range;
- applied in the correct amount and position.
It should also be remembered that some CuP alloys used on copper-copper can perform a self-deoxidizing action thanks to the presence of phosphorus and, under these conditions, do not normally require an additional deoxidizer.
Incorrect Amount of Solder
Using a higher amount of solder does not necessarily mean a stronger joint.
In properly designed brazing, the alloy should penetrate and distribute itself in the space between the components.
Excess material can increase costs and create external buildup without providing any real benefit to the strength of the joint.
An insufficient quantity, however, may result in incomplete filling.
How to avoid it
The quantity of alloy must be defined as a function of:
- surface to be brazed;
- joint geometry;
- play between components;
- alloy feeding mode.
In automated production, the use of rings, preforms or predetermined quantities of alloy can contribute significantly to process repeatability.
Movement of Components during Solidification
Once the alloy has filled the joint, the components must remain in the correct position until completely solidified.
Movement or vibration during this stage may interfere with the formation of the joint.
Possible consequences
- discontinuity;
- non-uniform joint;
- reduction of resistance;
- dimensional or alignment problems.
How to avoid it
It is advisable to use suitable positioning or fastening systems and wait for the alloy to solidify before moving the assembly.
Lack of Process Control
In industrial production, getting a good joint once is not enough.
The goal should be to achieve the same level of quality in a repeatable manner .
Seemingly small variables – such as heating time, flame position, amount of flux, or amount of alloy – can generate significant differences between components.
How to avoid it
When possible, it is useful to standardize:
- surface preparation;
- play and positioning of components;
- amount of alloy;
- quantity and method of application of the deoxidizer;
- thermal cycle;
- warm-up time;
- cooling mode;
- final checks.
Automating some phases can also help reduce operator-related variability.
Quick guide to the diagnosis of the main brazing defects
| Problem observed | Possible causes | What to check |
|---|---|---|
| The alloy does not wet the surface | Contaminated surface, oxidation, insufficient temperature, inadequate deoxidizer | Cleaning, temperature and choice of flux |
| The alloy melts but does not penetrate the joint | Incorrect play, uneven heating, contaminated surfaces | Joint geometry and heat distribution |
| Strong oxidation | Too high temperature, prolonged heating, insufficient protection | Thermal and deoxidizing cycle |
| Incomplete joint | Insufficient amount of alloy, insufficient capillarity, non-uniform temperature | Amount of alloy, play and heating |
| Excessive alloy accumulation | Too high quantity or poor capillary action | Alloy dosage and geometry |
| Fragile or weak joint | Unsuitable alloy, incorrect geometry, overheating or movement during solidification | Alloy, process and joint design |
| Non-repeatable results | Variable process parameters | Standardization and process control |
Note: The same defect can have multiple causes. Diagnosis should therefore consider the process as a whole, not a single isolated parameter.
Click here to download a Brazing Defects & Trouble Shooting Guide
Preventing defects means controlling the entire process
The quality of a braze does not depend on a single element.
A reliable joint is born from the correct combination of:
Surface preparation
↓
Joint design
↓
Choice of brazing alloy
↓
Choice and application of flux
↓
Heating control
↓
Correct feeding of the alloy
↓
Cooling and final inspection
The standardization of these phases is particularly important in industrial processes, where quality and repeatability must be guaranteed on thousands of components.
Conclusion
Many of the defects found in brazing do not depend on a single error, but on the interaction between materials, brazing alloy, flux, joint geometry and thermal cycle .
Identifying the real cause of the problem is therefore essential before modifying the process.
Correct surface preparation, adequate joint clearance, the choice of the most appropriate alloy and flux, and careful heating control significantly reduce the risk of defects and achieve a more stable and repeatable process.
In the industrial setting, this means not only improving the quality of the joint, but also reducing rework and scrap, increasing productivity and improving the reliability of the final component.
Thessco Solutions for Brazing
 The correct selection of filler materials is a fundamental part of the process.
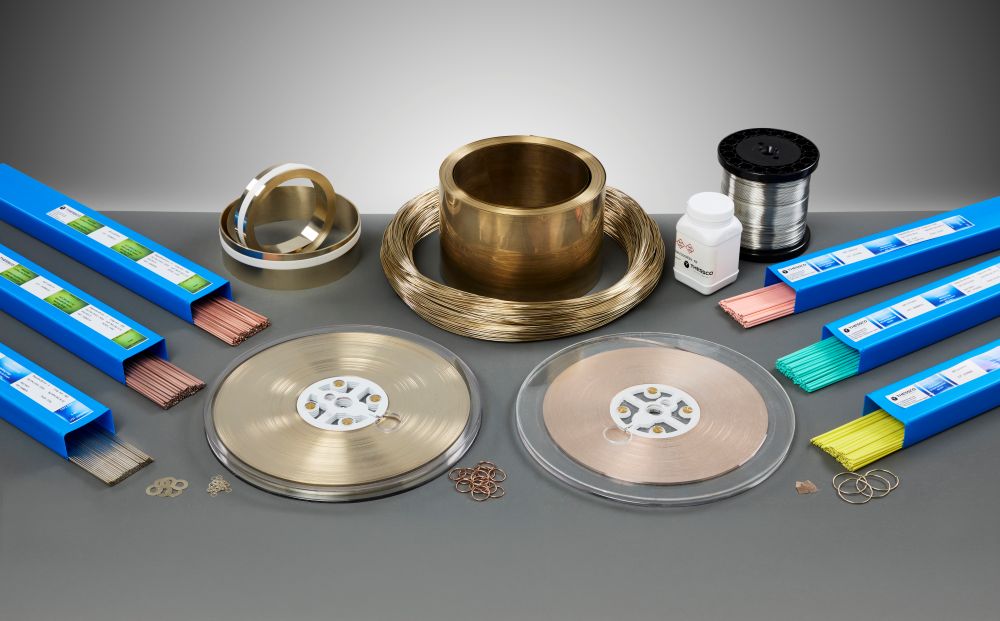
Thessco offers a complete range of solutions for different industrial applications:
- silver-based brazing alloys ;
- copper-phosphorus alloys (CuP) ;
- copper-phosphorus-silver alloys (CuPAg) ;
- brazing alloys available in different formats;
- Brazing fluxes, developed for different process needs;
- AGELCA Eco Green, the solution developed to combine high brazing performance with a formulation oriented towards greater attention to safety and sustainability.
Choosing the most appropriate combination of alloy, format, and flux can help improve the quality of the joint and the stability of the entire production process.